
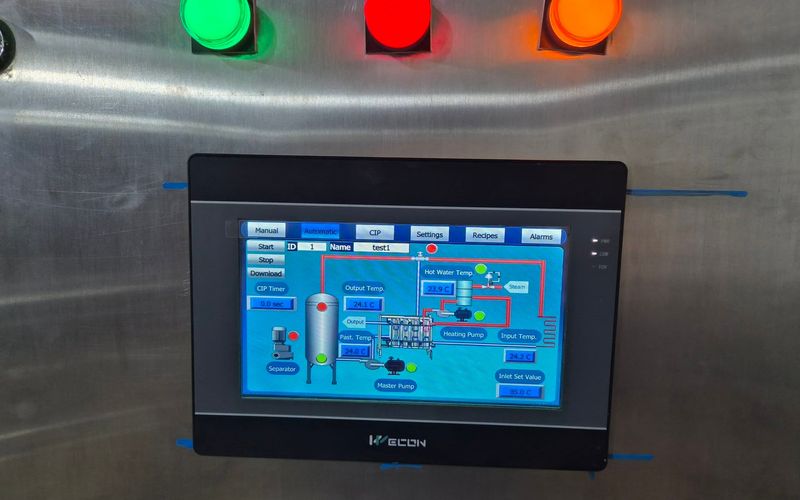
- Siemens · Schneider Electric · LS Electric · Wecon
Process control for thermal, CIP and batching systems
In food, dairy and pharma processes the product depends on the numbers: temperature, pressure, time, flow and dose. We build control systems that hold those numbers, stop the process when they are not met, and record what happened.
What our process control covers
Our process work includes pasteurizers with CIP, an olive sterilization autoclave, a cheese cooker, a tablet coating machine, a concrete batching plant, laundry dosing and a beverage syrup mixing system. Our engineers have also recommissioned purified-water utility systems in a pharmaceutical plant.
Temperature and pressure control
Closed-loop control of steam, hot water and heating, with setpoints for each product.
Time and phase control
Multi-phase cycles such as heating, holding, sterilizing and cooling, with time, temperature and pressure setpoints for each phase.
CIP sequences
Cleaning-in-place cycles with timed steps, pump and valve control, and their own screens on the HMI.
Batching and dosing
Weighing and dosing of raw materials, water, additives and chemicals, with mix recipes and batch sequences. Batch logic can be structured following ISA-88 principles.
Product-safety interlocks
Logic that holds or diverts product until process conditions are met, such as a pasteurizer flow-diversion valve.
Recipes and records
Recipes for each product, and data logging for quality records and traceability.
Live HMI demo
Run a pasteurizer from your browser
A working simulation of an HTST (high-temperature, short-time) milk pasteurizer, the kind of PLC and HMI system we build for dairy plants. Start it, change the recipe, cause a fault, run a CIP clean: the control logic reacts like the real machine.
Try it
- Press Start
- Wait for Forward
- Simulate a faultwatch TT-102
- Acknowledge the alarms
Press Start to run the pasteurizer.
TT-102 Holding outletFDV Divert
24.0°C
Divert limit ≥ 72.0 °C · min 15 s
PT-201 3.0 barTT-101 24.0 °C
- TT-101 Heater outlet
- 24.0 °C SP 72.5
- Holding time
- 0.0 s
- FT-101 Flow
- 0 L/h
- TT-201 Hot water
- 70.0 °C
- TCV-201 Steam valve
- 0 %
- Batch B-1041
- 0.0 L
Recipe
Forward permissive Blocked
- TT-102 ≥ 72.0 °C, not met
- Held for 2 s (check time), not met
- Regen ΔP: pasteurized > raw, not met
- Holding time ≥ 15 s, not met
Manual control
Heating SP
72.5 °C
FDV
CIP program
- Pre-rinse
- Caustic wash
- Intermediate rinse
- Acid wash
- Final rinse
Alarms & events
PriorityTimeTagMessageState
No active alarms
ISA-101Simulated 10.1″ operator panel designed following ISA-101 high-performance HMI principles: gray when all is normal, color only for abnormal states, blue for what you can touch.
When to call us for process control
- Temperatures or times vary between batches
- Operators adjust valves by hand
- Your quality team needs batch records
- A new process skid needs its control system
What you receive
- Written control description: sequences, interlocks and alarms
- Instrument and I/O list
- PLC and HMI or SCADA programs with recipes
- Loop checks and tuning at start-up
- Data logging set up as agreed
Related projects
Food and beverage2025
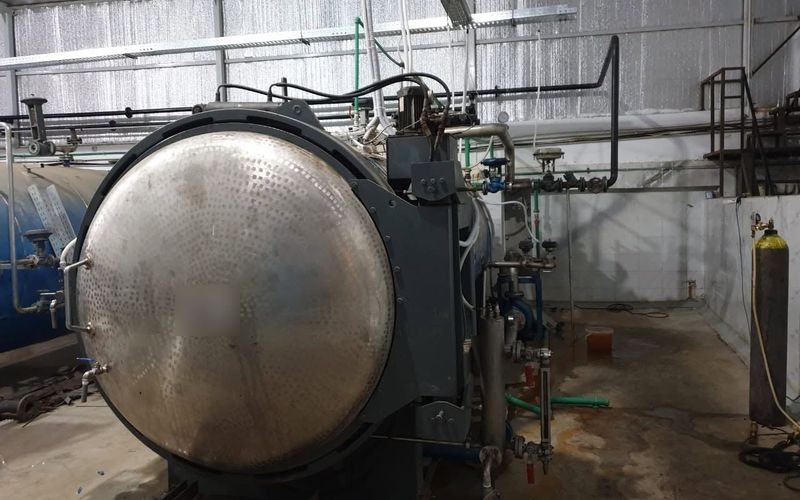
Olive sterilization autoclave on LS PLC
- LS Electric PLC with expansion module
- HMI
Building materials2025
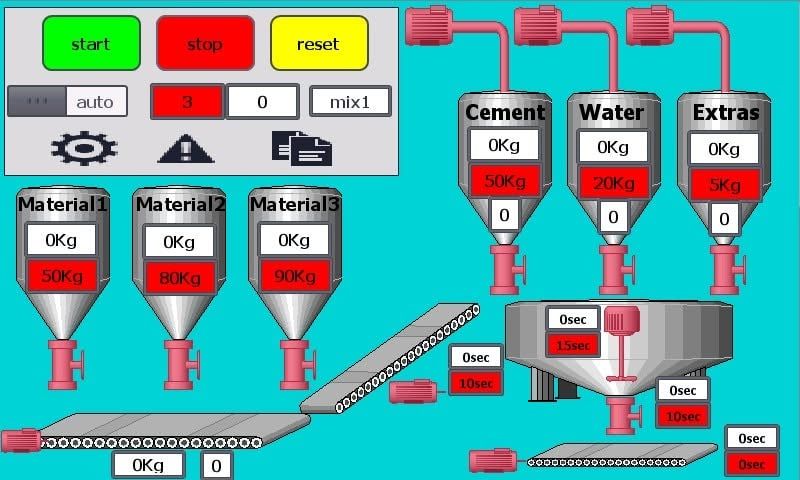
Concrete batching plant on Siemens S7-1200 and WinCC
- Siemens S7-1200 PLC
- Siemens WinCC Professional SCADA
Industries
Food and beverage
6 projectsPharmaceutical
1 projectBuilding materials
1 projectCommercial laundry
2 projects
Platforms we program and integrate
Brand names and logos belong to their owners. They are shown only to identify the hardware our engineers work with.
Frequently asked questions
Do you supply the instruments?
We specify sensors, transmitters and valves and can source them, or we work with the instruments already on your equipment. Every instrument is checked at commissioning.
Can the system keep records for quality audits?
Yes. Our process systems log key values and events, and the format is agreed per project. We do not provide formal computer-system validation, for example to 21 CFR Part 11.
Can you add CIP to an existing process?
Often, yes, if the valves and pumps allow it. CIP can run inside the machine program, as in our pasteurizer projects, or as a separate sequence.
Process control
Need tighter process control?
Describe the process, the setpoints you need to hold and the instruments you have. We will propose a control solution.
What we need to quote
You do not need everything on this list. Send what you have and we will ask for the rest.
- What the machine or line does, and what you want to change
- Photos of the machine, the existing panel and the nameplates of the motors, drives and PLC
- Drawings, an I/O list or the existing program, if you have them
- Preferred PLC and HMI brand, or no preference
- Supply voltage and frequency at the machine, for example 380 V, 50 Hz
- Plant location and target date
- Languages needed for the HMI screens and documents