Skip to content
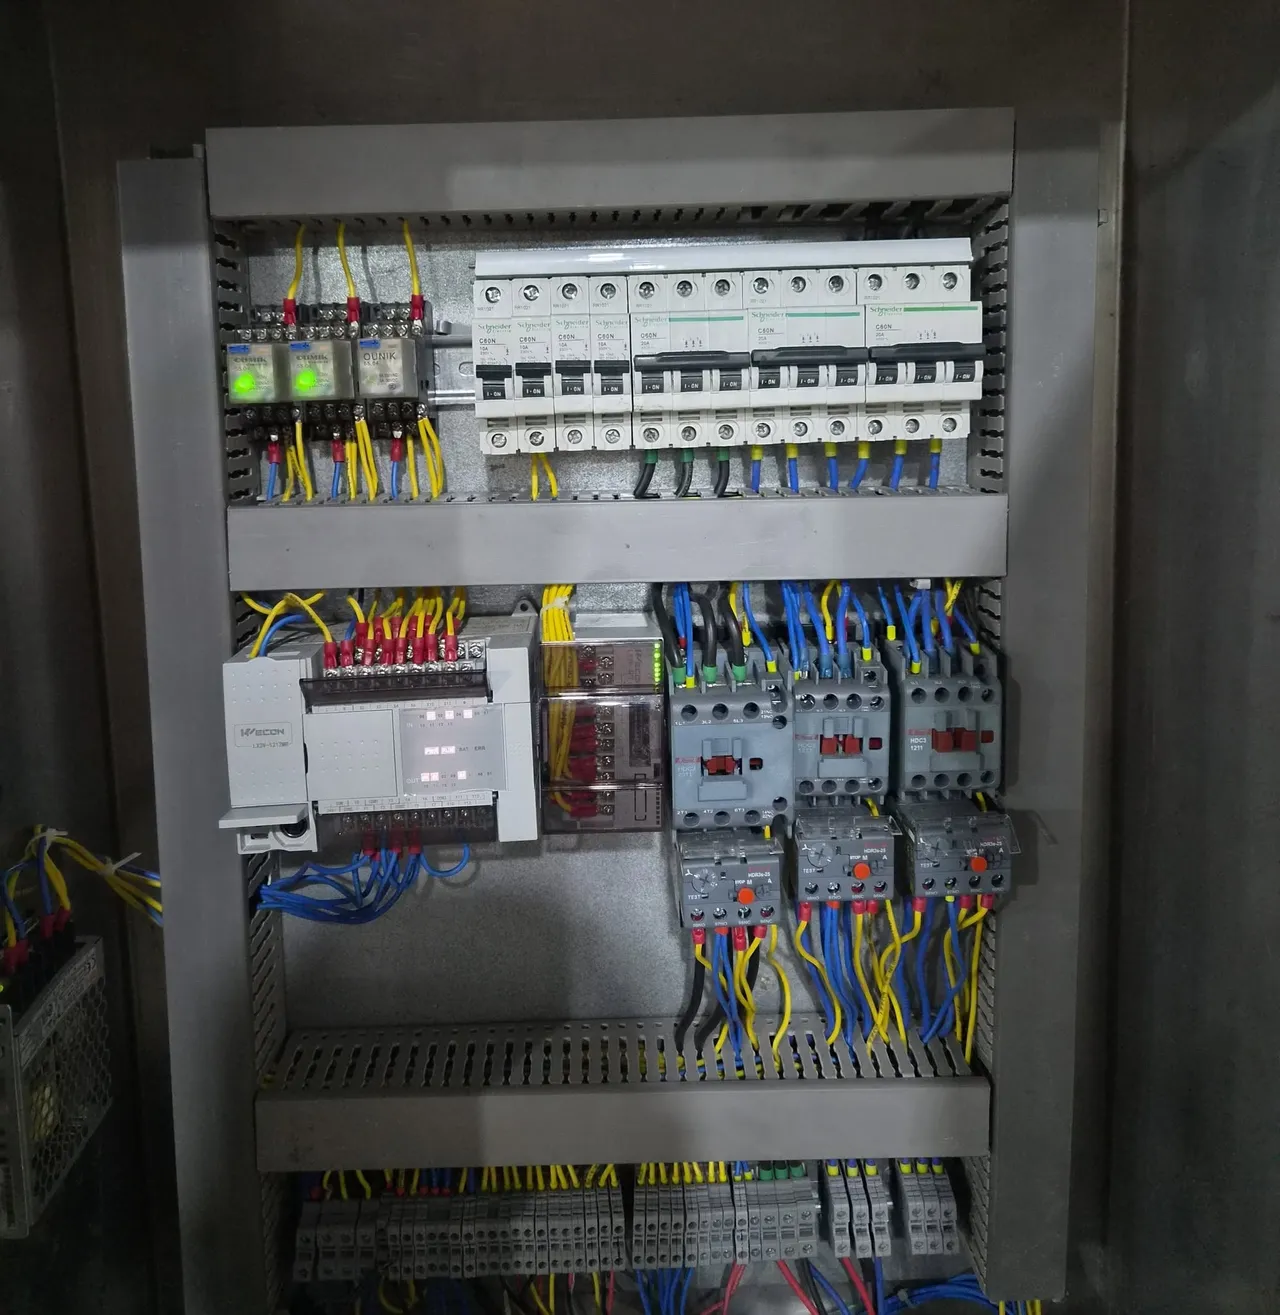
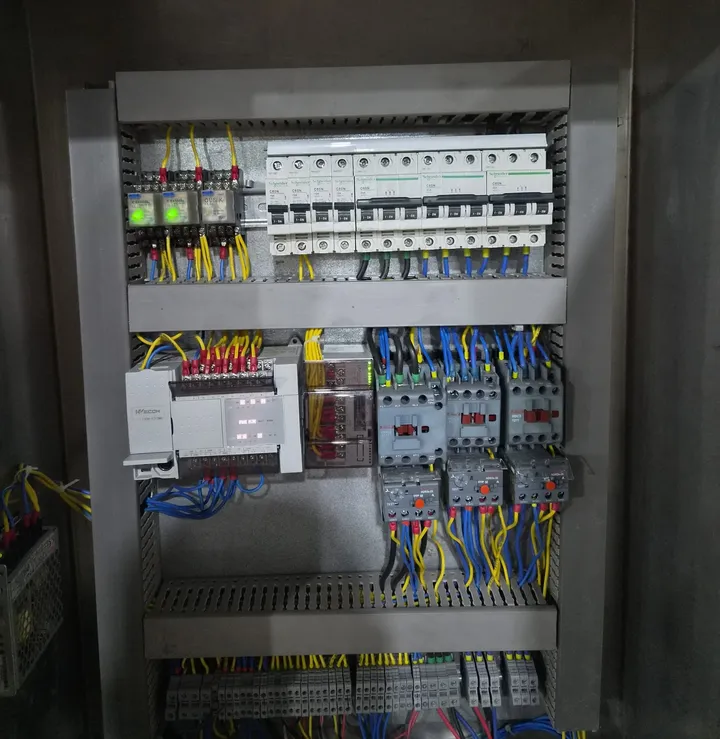
Pasteurizer control panel with Wecon PLC, Schneider Electric circuit breakers, relays, contactors and overload relays
  • PLC · HMI · SCADA · VFD

PLC, HMI and SCADA platforms we program and integrate

We are not tied to one brand. We program and integrate five PLC and HMI platforms and choose the one that fits your machine, your budget and the spare parts you can get in Egypt.

01PLC · HMI

PLC and HMI platforms we program and integrate

Below are the platforms, drives, software and signals we work with, and the products we have used in recent projects.

Siemens

S7-1200 PLCs with WinCC Professional SCADA for process machines and plants, as in our tablet coating and concrete batching projects, and with a SIMATIC HMI on our beverage syrup mixing system. We have also commissioned S7-200 SMART systems.

Used in our projects

  • S7-1200
  • WinCC Professional
  • SIMATIC HMI
  • S7-200 SMART

Schneider Electric

PLCs, Altivar variable-speed drives, stepper drives, and protection and control components. Schneider Electric stepper drives run the label dispensing on our labeling machine.

Used in our projects

  • Altivar VFDs
  • Stepper drives
  • C60N circuit breakers

Delta

DVP-series PLCs for filling and labeling machines, chosen where a compact, cost-effective controller fits the job.

Used in our projects

  • DVP-series PLCs

LS Electric

PLCs for filling machines and sterilization autoclaves, and M100 variable-speed drives.

Used in our projects

  • PLCs
  • M100 VFD

Wecon

PLCs and touch-screen HMIs used in most of our machine projects: pasteurizers, a cheese cooker, laundry washers, filling, labeling and test machines.

Used in our projects

  • LX3V PLCs
  • HMIs

02By category

Drives, SCADA, networks and signals

The controller is only one part of the system. These are the other layers we design, program and commission around it.

Drives and motion

Variable-speed drives for conveyors, pumps, mixers, drums and fans, and stepper and motion control for positioning and synchronization.

  • LS Electric M100 VFDs
  • Schneider Electric Altivar VFDs
  • VEICHI VFDs
  • Yaskawa VFDs
  • Schneider Electric stepper drives
  • PLC-based motion control for synchronized positioning

Software, SCADA and data

From electrical drawings in EPLAN Electric P8 to a single touch screen on a machine or a SCADA overview of a full process.

  • EPLAN Electric P8 for electrical design and panel drawings
  • Siemens WinCC Professional SCADA
  • SQL database integration for SCADA reports and OEE dashboards
  • Process mimics, recipes and alarm history on HMIs
  • Arabic, English and bilingual HMI screens
  • User log-in and access levels
  • Data logging and automatic test reports

Communication

We connect PLCs, HMIs, drives and instruments over common industrial networks. We check every device's interface before we quote.

  • Modbus RTU over RS-485
  • Modbus TCP
  • PROFINET for Siemens systems
  • Industrial Ethernet with managed and unmanaged switches

Signals and instruments

  • Digital inputs and outputs: sensors, switches, valves and contactors
  • Analog signals: 4-20 mA and 0-10 V transmitters and positioners
  • Temperature sensors: RTD and thermocouple
  • Weighing with load cells for batching
  • Encoders and fast counters for length and position
  • Level, pressure and gas measurement on process systems

How automation works

The control loop behind every machine

Sensors measure, the PLC decides, the HMI keeps people in the loop and the actuators act. Then it starts again, many times a second.

  1. Sensor

    Measures the process: temperature, pressure, level, flow or position.PT100 · 4–20 mA
  2. PLC

    Compares the value with the setpoint and runs the logic: PID, interlocks, sequences.PID · 10 ms scan time
  3. HMI / SCADA

    Shows operators live values, alarms and trends, and passes their commands to the PLC.Modbus TCP
  4. Actuator

    A VFD, control valve or contactor applies the PLC's output to the machine.VFD 0–50 Hz
  5. Process

    The machine responds, and the sensor measures the new value.72.4 °C

Signal types shown are typical examples.

Live HMI demo

Run a pasteurizer from your browser

A working simulation of an HTST (high-temperature, short-time) milk pasteurizer, the kind of PLC and HMI system we build for dairy plants. Start it, change the recipe, cause a fault, run a CIP clean: the control logic reacts like the real machine.

Try it

  1. Press Start
  2. Wait for Forward
  3. Simulate a faultwatch TT-102
  4. Acknowledge the alarms
Logic Controls
HTST-01 PasteurizerOverview
Mode: AUTOStatus: Ready0 unacknowledgedSimulation at 3× real time
RegenHeatingCoolingFT101TT101TT102TT103TT201PT20182.0 %50.0 %18.0 %0 L/h24.0 °C24.0 °C6.0 °C70.0 °C3.0 bar0 %312724 °C90 °CRaw tankT-101LV-101B-101Balance tankFeed pumpP-101Plate heat exchangerHolding tube0.0 sFDV-101DivertForward ←Divert ←StorageT-301HW pumpHot waterIce waterSteamTCV-201CIP supply

Press Start to run the pasteurizer.

TT-102 Holding outletFDV Divert
24.0°C
Divert limit ≥ 72.0 °C · min 15 s

PT-201 3.0 barTT-101 24.0 °C

TT-101 Heater outlet
24.0 °C SP 72.5
Holding time
0.0 s
FT-101 Flow
0 L/h
TT-201 Hot water
70.0 °C
TCV-201 Steam valve
0 %
Batch B-1041
0.0 L

Recipe

Forward permissive Blocked

  • TT-⁠102 ⁦≥ 72.0 °C⁩, not met
  • Held for ⁦2 s⁩ (check time), not met
  • Regen ΔP: pasteurized > raw, not met
  • Holding time ⁦≥ 15 s⁩, not met

Manual control

Heating SP
72.5 °C
FDV

CIP program

  1. Pre-rinse
  2. Caustic wash
  3. Intermediate rinse
  4. Acid wash
  5. Final rinse

Alarms & events

PriorityTimeTagMessageState
No active alarms

ISA-101Simulated 10.1″ operator panel designed following ISA-101 high-performance HMI principles: gray when all is normal, color only for abnormal states, blue for what you can touch.

Want an HMI like this for your machine?

Request a quoteSee the real pasteurizer we automated

03Our approach

How we choose a platform

  1. Spare parts in Egypt

    A controller is only as good as the replacement you can buy when it fails.

  2. Your budget

    Cost-effective platforms for simple machines, and higher-end PLCs and SCADA where the process needs them.

  3. Your team

    If your maintenance team already knows one brand, we take that into account.

  4. The machine builder's standard

    For imported or OEM machines, we follow the platform the machine was designed for, unless there is a reason to change.

Tell us about your machine or line

Send a short description and a few photos. An engineer will review it and reply with questions or a quote.

Phone: +20 110 319 7233Email: info@logic-controls.com

Phone: +20 110 319 7233