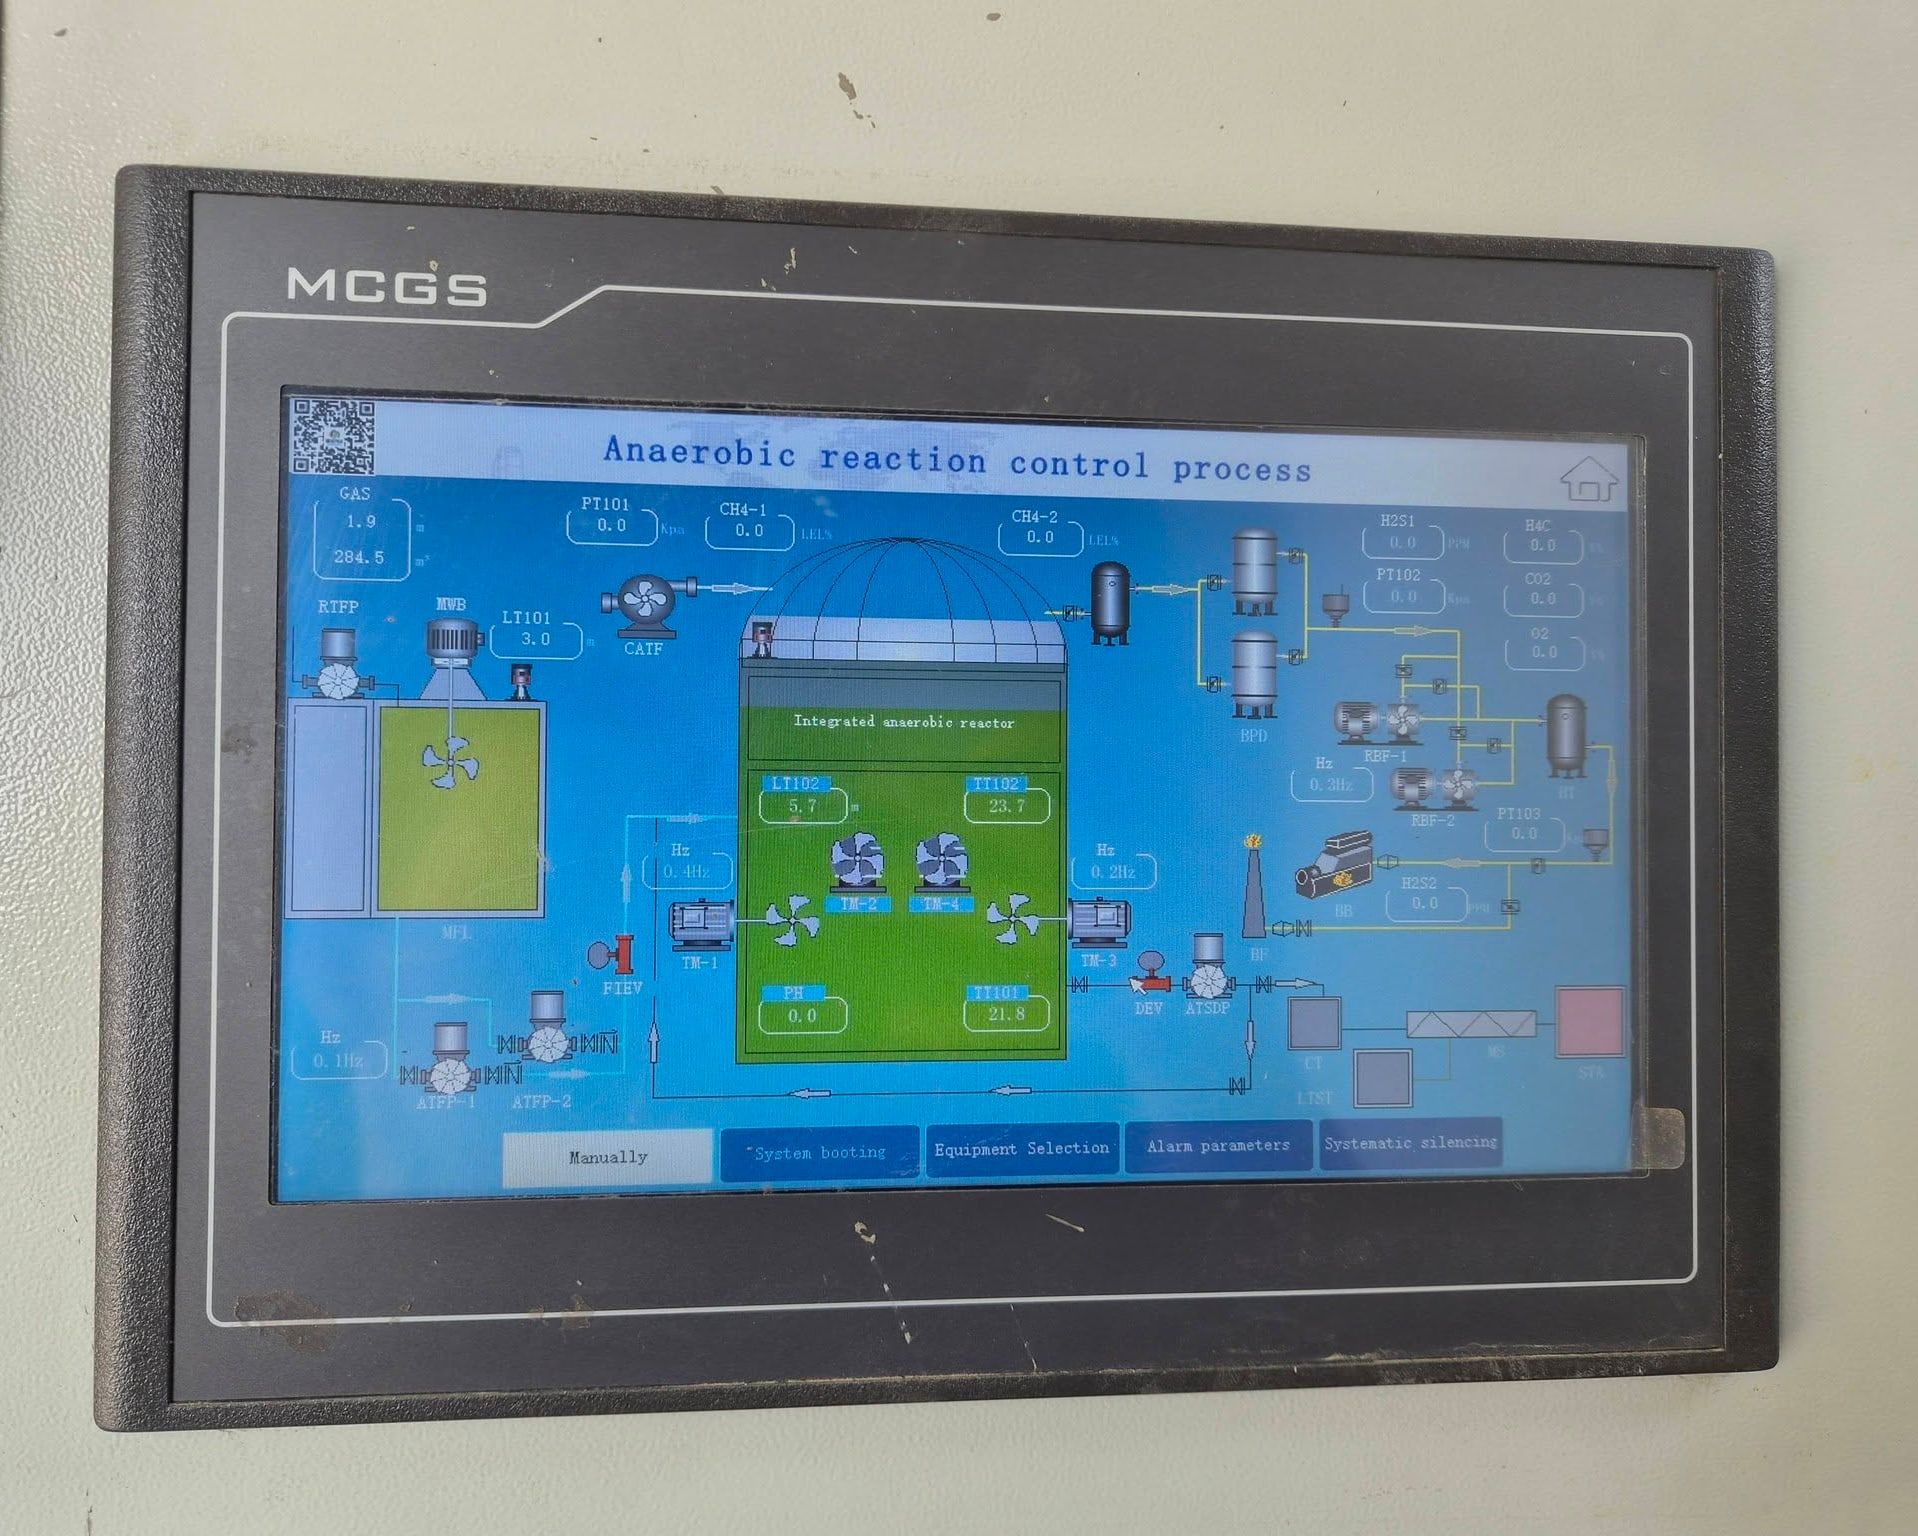
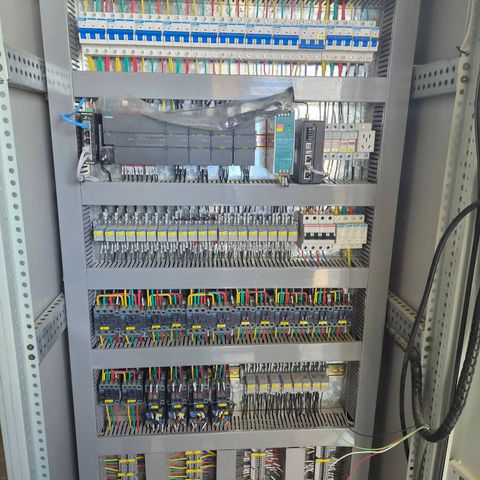
Factories and machine builders in Egypt
New machines, upgrades of old ones, breakdowns and process improvements. Engineers who speak your language and come to your site.
Animations are off because your device is set to reduce motion.
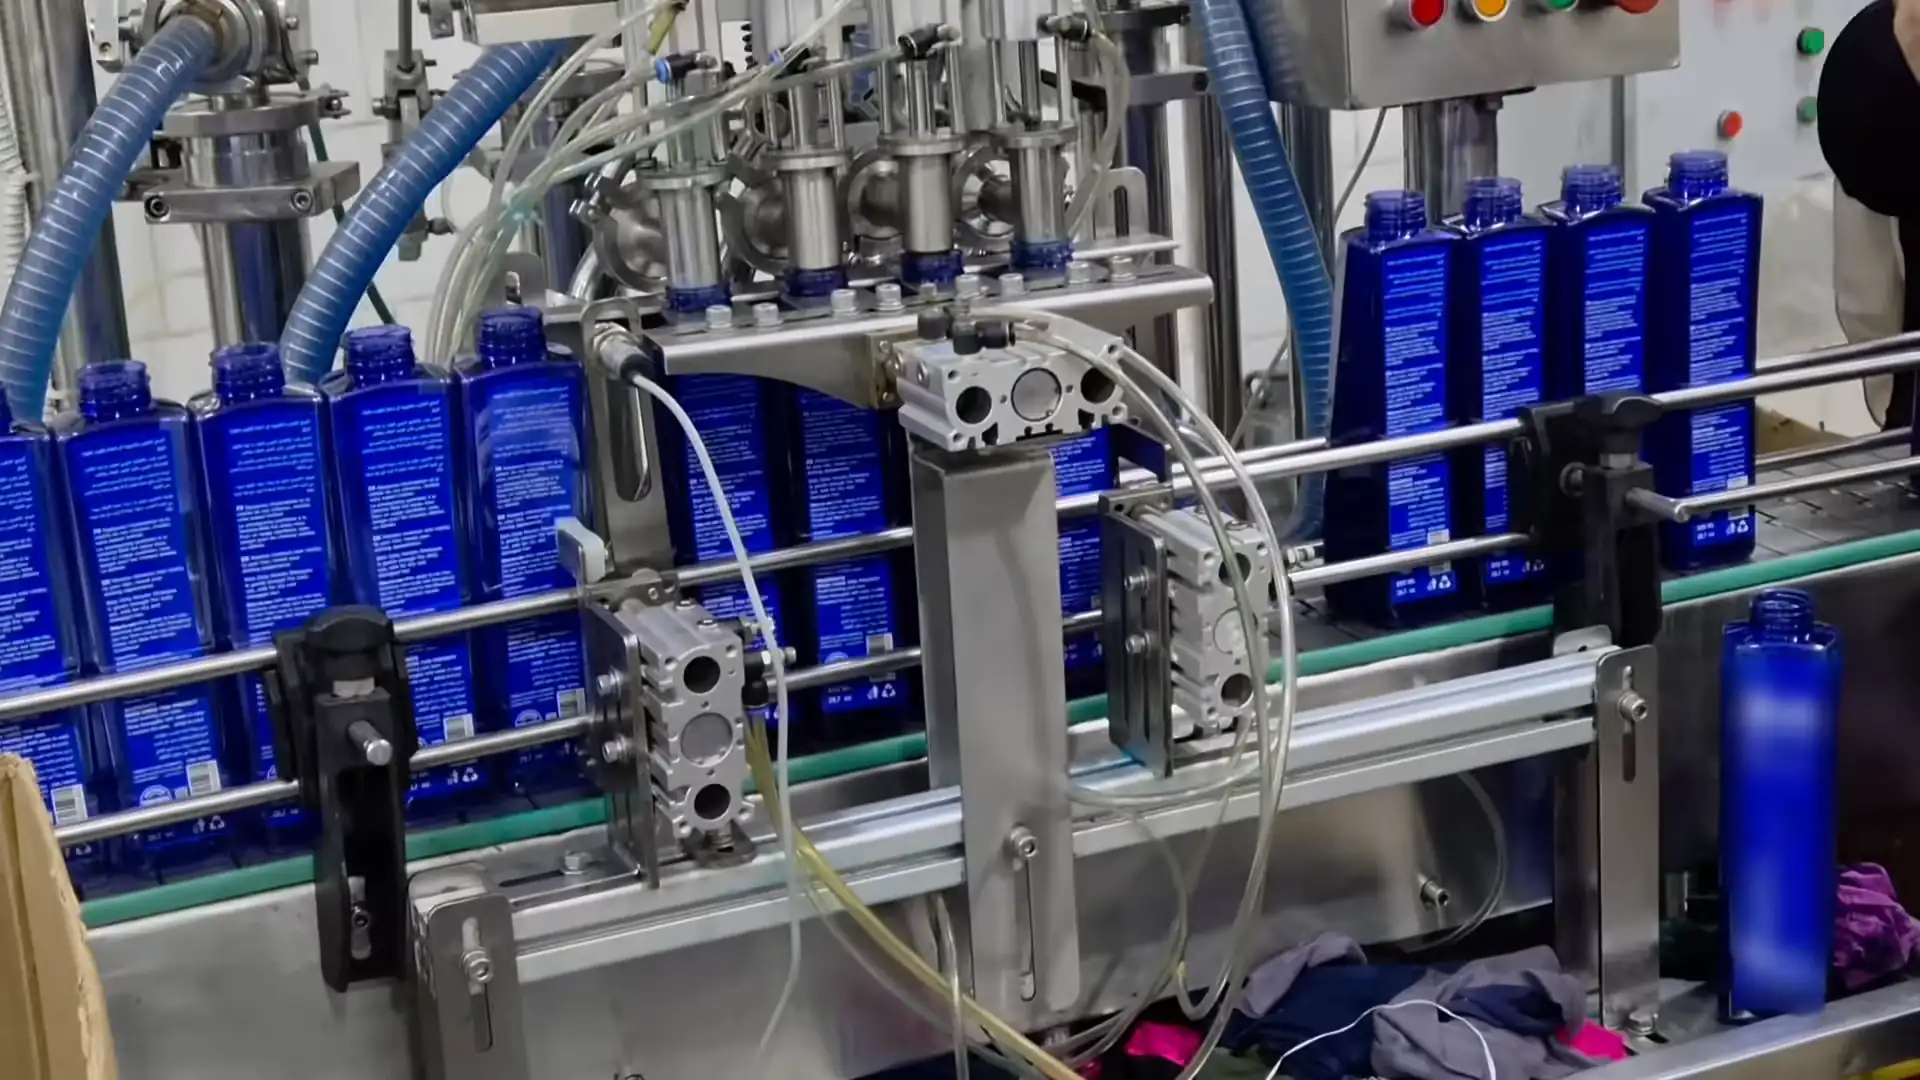
We design the control system, program the PLC, HMI and SCADA, and commission the machine on your floor. For food, dairy, pharma, cosmetics and packaging lines.
Platforms we program and integrate
We choose the platform that fits your machine, your budget and the spare parts you can get in Egypt.
See technologiesBrand names and logos belong to their owners. They are shown only to identify the hardware our engineers work with.
New machines, upgrades of old ones, breakdowns and process improvements. Engineers who speak your language and come to your site.
A local engineering team to commission imported lines, put HMI screens in Arabic for your operators and support the plant after start-up.
01Featured projects
Real machines and real photos from our projects. Client names are withheld.
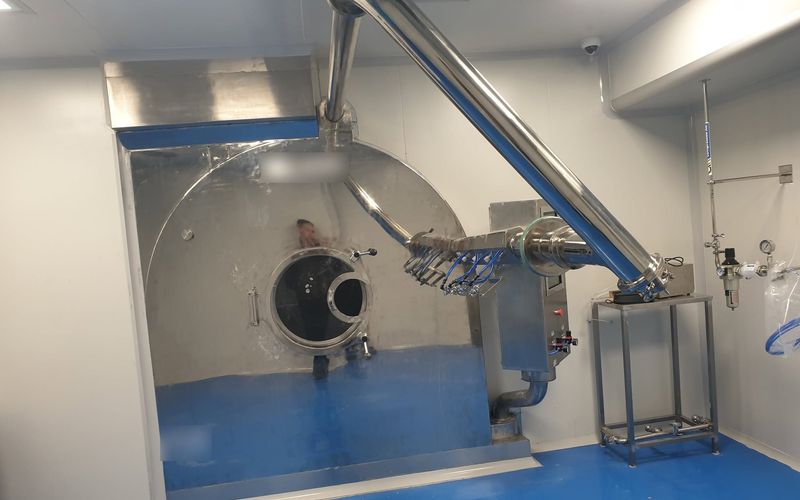
Pharmaceutical2025
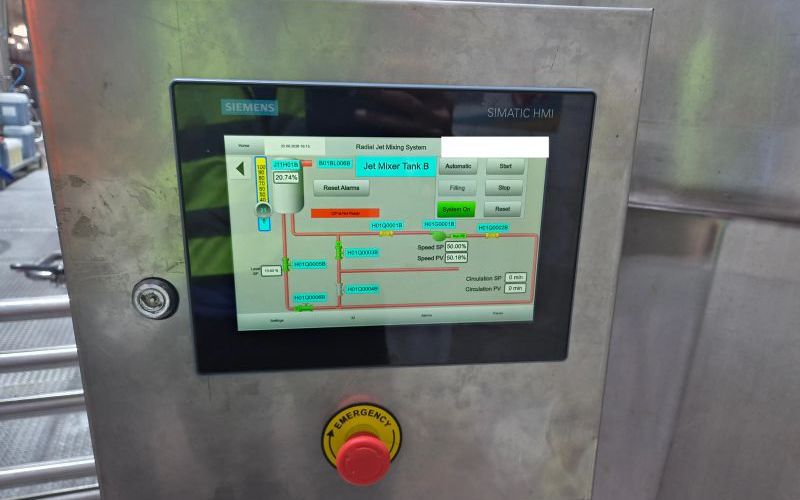
Food and beverage2026
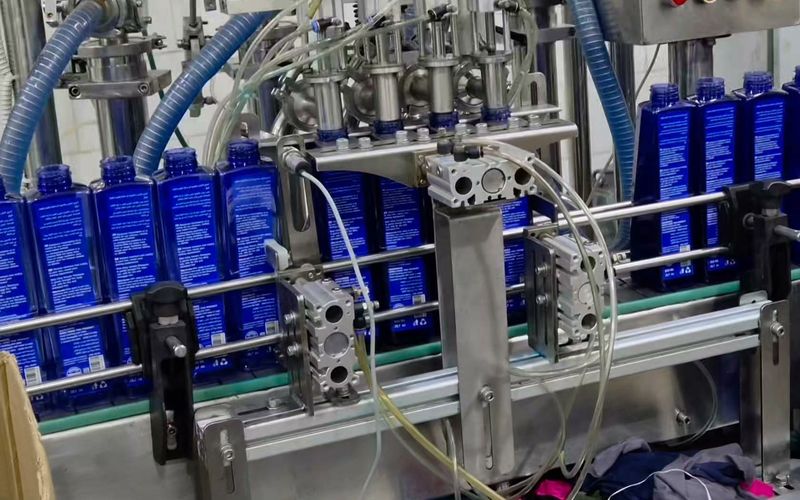
Client names are withheld for confidentiality. References can be arranged on request, with the client's permission.
02Services
Eight services, from electrical design and panels to commissioning and support. Take the full scope or only the part you need.
Schematics, I/O lists and PLC control panels, designed, assembled, wired and tested for your machine or process.
Clear, commented PLC logic and HMI screens for Siemens, Schneider Electric, Delta, LS Electric and Wecon, in Arabic, English or both.
Complete control systems for filling, labeling, printing, washing and test machines: PLC, HMI, VFDs, stepper and motion control.
Keep a good machine and replace its old controls: new PLC, HMI, drives and motion control, documented and tested, with a planned changeover.
Control of pasteurization, sterilization, cooking, coating, CIP, batching and dosing, with recipes, interlocks and data logging.
SCADA screens, alarms, recipes, reports and traceability, so you can see the process and show what was produced.
I/O and loop checks, interlock tests, start-up and tuning, for systems we build and for machines and lines supplied by others.
Breakdown troubleshooting, program changes, preventive maintenance, operator training and help sourcing spare parts in Egypt.
03Industries
Most of our work is in plants where temperature, time, dose or position decides product quality.
04Why choose us
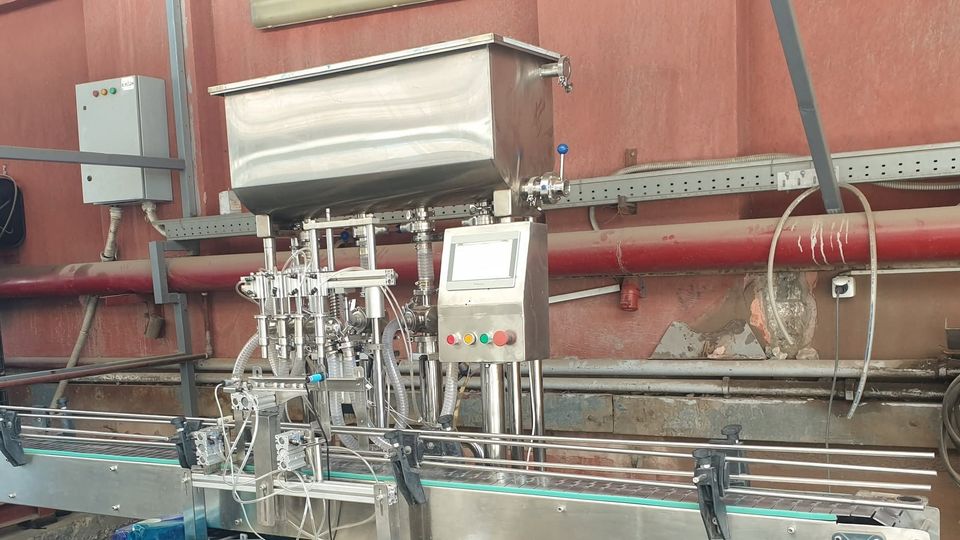
The engineer who designs your control system also programs it and commissions it. Nothing is lost between teams.
Siemens, Schneider Electric, Delta, LS Electric and Wecon. We recommend the platform that fits your budget, your spare parts and your maintenance team.
HMI screens in Arabic, English or both, with clear alarms, manual and automatic modes, and recipes operators can select.
Every I/O point, interlock and alarm is checked before production. You receive drawings and notes your maintenance team can use.
Who you will work with
You talk directly to the automation engineers who work on your system, not to a sales middleman. Our team has more than four years of experience designing, programming and commissioning PLC, HMI and SCADA systems for food and beverage, pharmaceutical and other plants.
About us05From survey to handover
Six steps from the first visit to a running machine. You talk to the same engineers throughout.
We see the machine or line, read the nameplates and drawings, and agree what the system must do.
You receive a written scope and quote. Once agreed, we produce the schematics, I/O list and bill of materials.
We assemble and wire the control panel, write the PLC program and design the HMI screens.
Wiring checks, I/O simulation and an HMI walk-through before anything reaches your floor.
I/O and loop checks, interlock tests, start-up and tuning with your operators.
As-built drawings, operator training and follow-up support when you need changes.
Testing and commissioning
We commission imported lines, run I/O and loop checks, build Arabic HMIs for local operators and support the plant after start-up.
Food and beverage manufacturer · 2026
06Location
We are based in 6th of October City, Giza. We work across Greater Cairo and Egypt's industrial zones, including:
Our base: 6th of October and New October
6th of October and New October
10th of Ramadan City
About 90 km from our base (straight line)
Plan a project in 10th of RamadanRequest a quoteBorg El Arab and New Borg El Arab
About 160 km from our base (straight line)
Plan a project in Borg El ArabRequest a quoteAin Sokhna, including the TEDA zone
About 140 km from our base (straight line)
Plan a project in Ain SokhnaRequest a quoteEast Port Said
About 200 km from our base (straight line)
Plan a project in East Port SaidRequest a quoteAbout 60 km from our base (straight line)
Plan a project in Obour CityRequest a quoteAbout 75 km from our base (straight line)
Plan a project in Badr CityRequest a quoteAbout 90 km from our base (straight line)
Plan a project in 10th of RamadanRequest a quoteAbout 60 km from our base (straight line)
Plan a project in Sadat CityRequest a quoteAbout 160 km from our base (straight line)
Plan a project in Borg El ArabRequest a quoteAbout 140 km from our base (straight line)
Plan a project in Ain SokhnaRequest a quoteAbout 160 km from our base (straight line)
Plan a project in Qantara WestRequest a quoteAbout 200 km from our base (straight line)
Plan a project in East Port SaidRequest a quotePlant somewhere else in Egypt? Ask us. We plan site visits case by case.
07Frequently asked questions
Send a short description and a few photos. An engineer will review it and reply with questions or a quote.
You do not need everything on this list. Send what you have and we will ask for the rest.